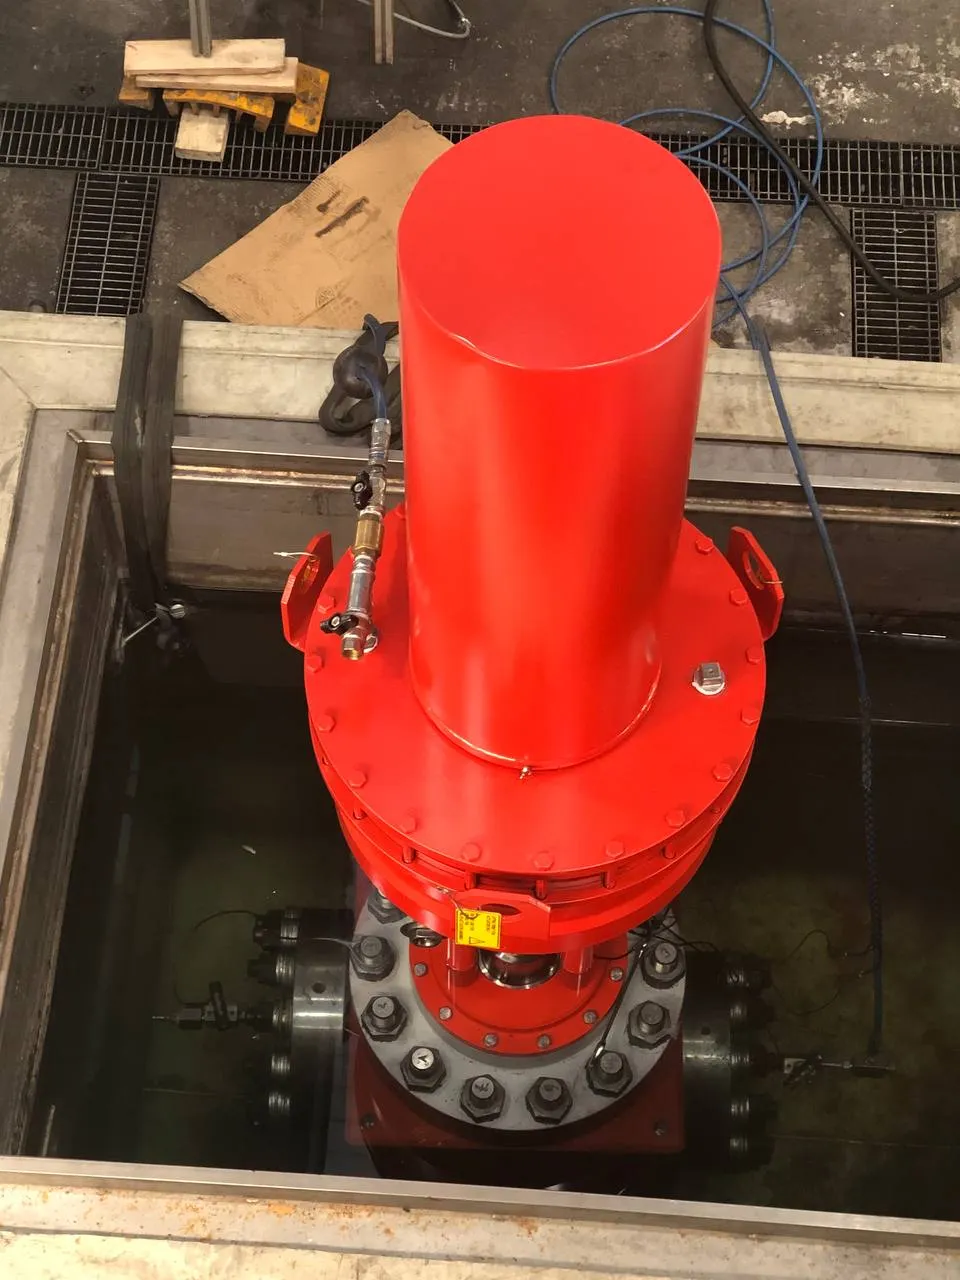
Why the factory test is decisive
A valve that leaks in the plant means a shutdown, removal and often replacement. The factory pressure test is the only moment when body, seals and closure member are verified under controlled conditions against written acceptance criteria. That is why the purchase order almost always names a test standard and the ITP includes a Witness or Hold point for the inspector.
The main tests
The three standards use different names, but the basic tests are the same:
Shell test
Valve partly open, body and bonnet pressurised with liquid, normally at 1.5 times the rated pressure at ambient temperature. No visible leakage is allowed through the body or joints.
Seat (closure) test
Valve closed, pressure applied on one side and leakage measured on the other. It is done with liquid (about 1.1 times the rated pressure) or with low-pressure gas (about 4–7 bar), depending on the standard and the valve type.
Backseat test
Only for valves with a stem backseat (e.g. gate and globe valves): it checks that the stem seals against the bonnet, so the packing can be serviced in operation.
The three standards side by side
A practical summary. When in doubt, the text of the standard in the edition named in the order always prevails.
| Aspect | API 598 | ISO 5208 | EN 12266-1 |
|---|---|---|---|
| Where it is used | Oil & gas and petrochemical, API valves (API 600, 602, 608, 609, 594…) | General international standard for industrial metallic valves | Valves built to EN standards, often in the context of the PED |
| Shell test | Liquid, 1.5 × rated pressure at 38 °C | Liquid, 1.5 × PS | Test P10 (shell strength) and P11 (shell tightness) |
| Seat test | Low-pressure gas and/or high-pressure liquid, depending on the valve type | Liquid at 1.1 × PS or gas at about 6 bar | Test P12, liquid or gas |
| Seat acceptance criteria | Table by size: zero visible leakage for soft seats; drops or bubbles per minute allowed for larger metal seats | Leakage rates (Rate A, B, C, D…): the rate is chosen by the order or the product standard | Leakage rates (Rate A, B, C, D…) called up by the EN product standard |
| Minimum duration | From a table, depending on size (NPS) | From a table, depending on size (DN) | From a table, depending on size (DN) |
PS = maximum allowable pressure at ambient temperature. Rate A means no visible leakage for the whole test duration.
Which standard applies?
Neither the inspector nor the supplier chooses it: it is set by the purchase order, the client specification and the valve's product standard. An API 600 valve is normally tested to API 598; a valve built to an EN standard calls up EN 12266-1. If the order quotes two standards, or a leakage rate that does not suit the seat type, clarify it in writing before the test, not in front of the test bench.
What the inspector checks at the test bench
A checklist to use when witnessing the tests. Adapt it to your project ITP.
1. Before starting
- Valve identification: nameplate, serial number and markings match the order and the material certificate
- Approved test procedure with pressures, fluid, durations and acceptance criteria
- Calibrated pressure gauges with a valid certificate and a range suited to the test pressure
- Valve not painted on the areas to be checked, with no sealant or grease that could hide leaks
- Test water quality (e.g. chloride content for austenitic stainless steels) as per specification
2. During the shell test
- Test pressure calculated from the ambient-temperature rating, not the rating at design temperature
- Air vented, valve partly open, duration counted only once the pressure is stable
- Inspection of body, bonnet, joints and stem seal for the whole duration
3. During the seat test
- Valve closed with normal operating force, without extra levers or wrenches
- Test in the required direction; for bidirectional valves, in both directions
- Leakage measured with a suitable method (drop or bubble count, volumetric measurement) and compared with the required rate
- For double block and bleed valves: each seat verified through the body cavity bleed
4. After the test
- Valve drained and dried, end protectors fitted
- Actual values recorded in the report: pressures, durations, measured leakage, gauge serial number
- Test marking or tag applied to the valve, when required
The non-conformities we find most often
- Gauge with expired calibration, or a range too large to read the pressure accurately
- Test duration shorter than the minimum, or counted before the pressure stabilised
- Valves already painted before the shell test
- Leakage rate in the report different from the one required by the order
- Reports showing "OK" instead of the measured values
What you receive from us
An inspection report with photos, measured values for each valve or batch, any NCRs with the reference requirement and, when everything conforms, the Inspection Release Note for shipment.
Our valve inspection service